 Production control Marrari
Production Controller – Pro X
- OEEavailability × performance × quality
- Stopslogged with reason and operator
- Appproduction and targets on phone and TV
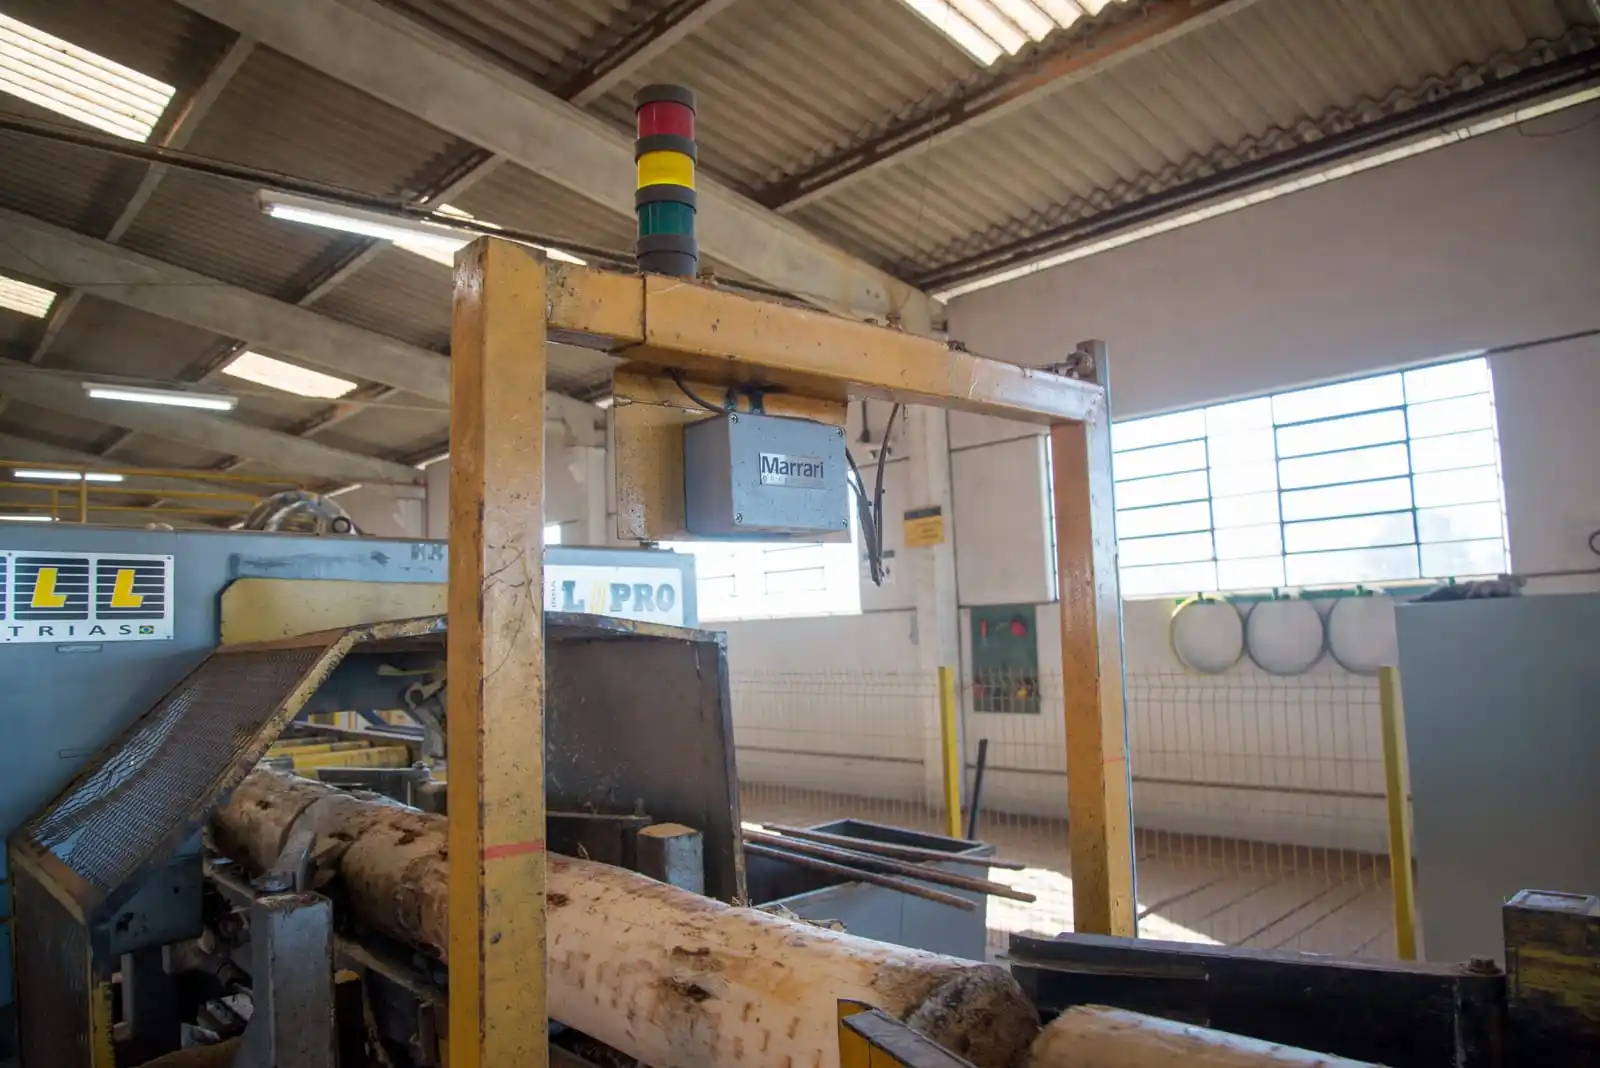
What is the Pro X production controller?
- Fits countless products and lines
0.1 mm resolution
- For whomSawmills, production lines and conveyors
- MeasuresLength, width, thickness, speed and pieces per minute
- ManagementOEE, stops with reasons and reports by batch, supplier and shift
- ProductionIn meters, m² and m³, against daily, weekly and monthly targets
Why control production in real time?
Without data, the target is a guess and every stop is a mystery. With every piece counted and every stop logged with its reason, the team knows right away whether the line is on target and where it loses efficiency. See why production control matters.
- OEE at a glance: machine availability, performance and quality in a single percentage.
- Stops with reasons: every stop logged, with the operator, to fix the cause.
- Targets met: the shop floor follows the target set by the manager in the software.
Where does your shift lose efficiency?
You do not need to know your line’s OEE:

- Availability
- Performance
- Quality
- OEE
Each loss in the shift falls into one of the 3 OEE factors, and
Simulation Example values, not readings from equipment.
Where is Pro X installed?
In any process that needs to count and measure pieces and control machines and lines, longitudinally or transversally. It can sit at several points in the plant; engineering helps you choose.
Basic · Standard · Carro · Sawmills · Conveyors · Production lines
- Basicpiece count or linear meters.
- Standardlogs and boards on a continuous line.
- Carrolog carriage.
- Sawmillssawmill output in m³ and by shift.
- Conveyorscounting and measuring pieces on the conveyor.
- Production linesquality and efficiency control, with data for management.
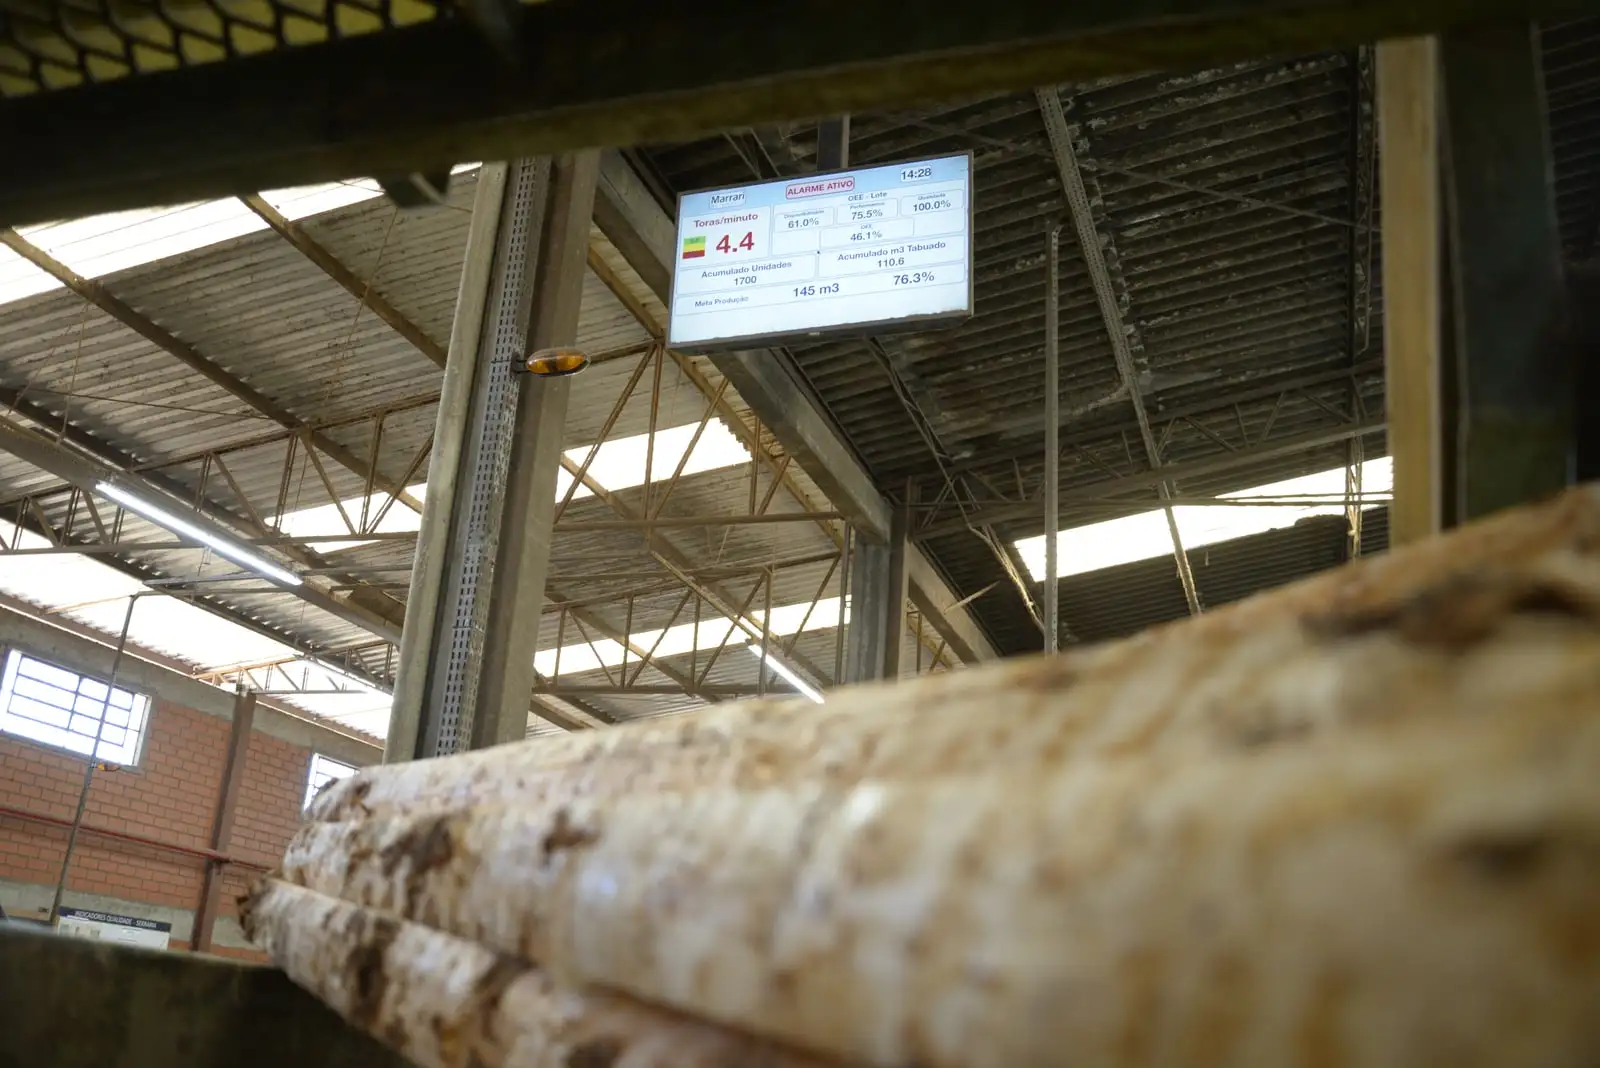
How does measurement work?
Optical laser sensors read each piece in
- Reads every piece
Laser from 50
to 650 mm, with0.1 mm resolution. - Measures and counts
Dimensions, speed, pieces per minute and volume produced.
- Logs stops
With the reason and the operator, for the OEE calculation.
- Shows and reports
Dashboard, TVs, app and reports by batch, supplier and shift.
Production control software: what does Pro X show on the computer?
On the computer,
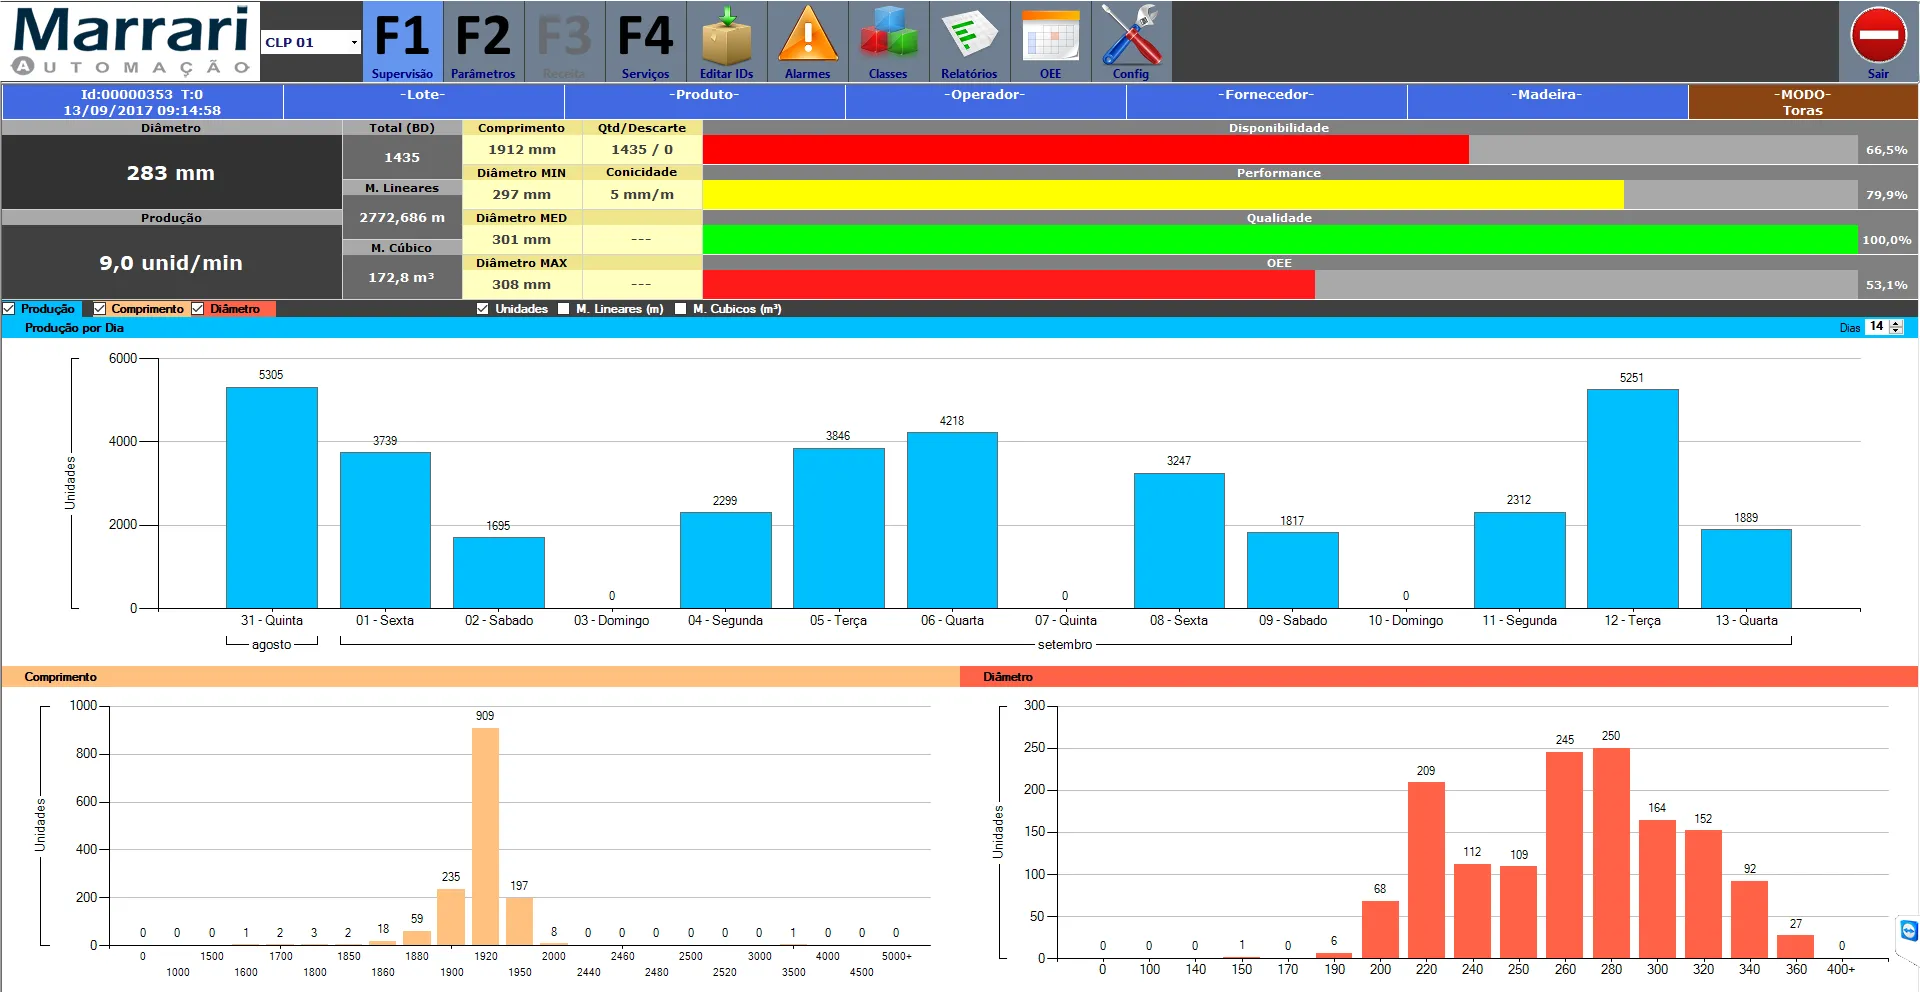
How to read this screen
- At the top, output per minute and the availability, performance, quality and OEE bars.
- In the middle, each day’s production, in columns.
- At the bottom, pieces split by length and by diameter.
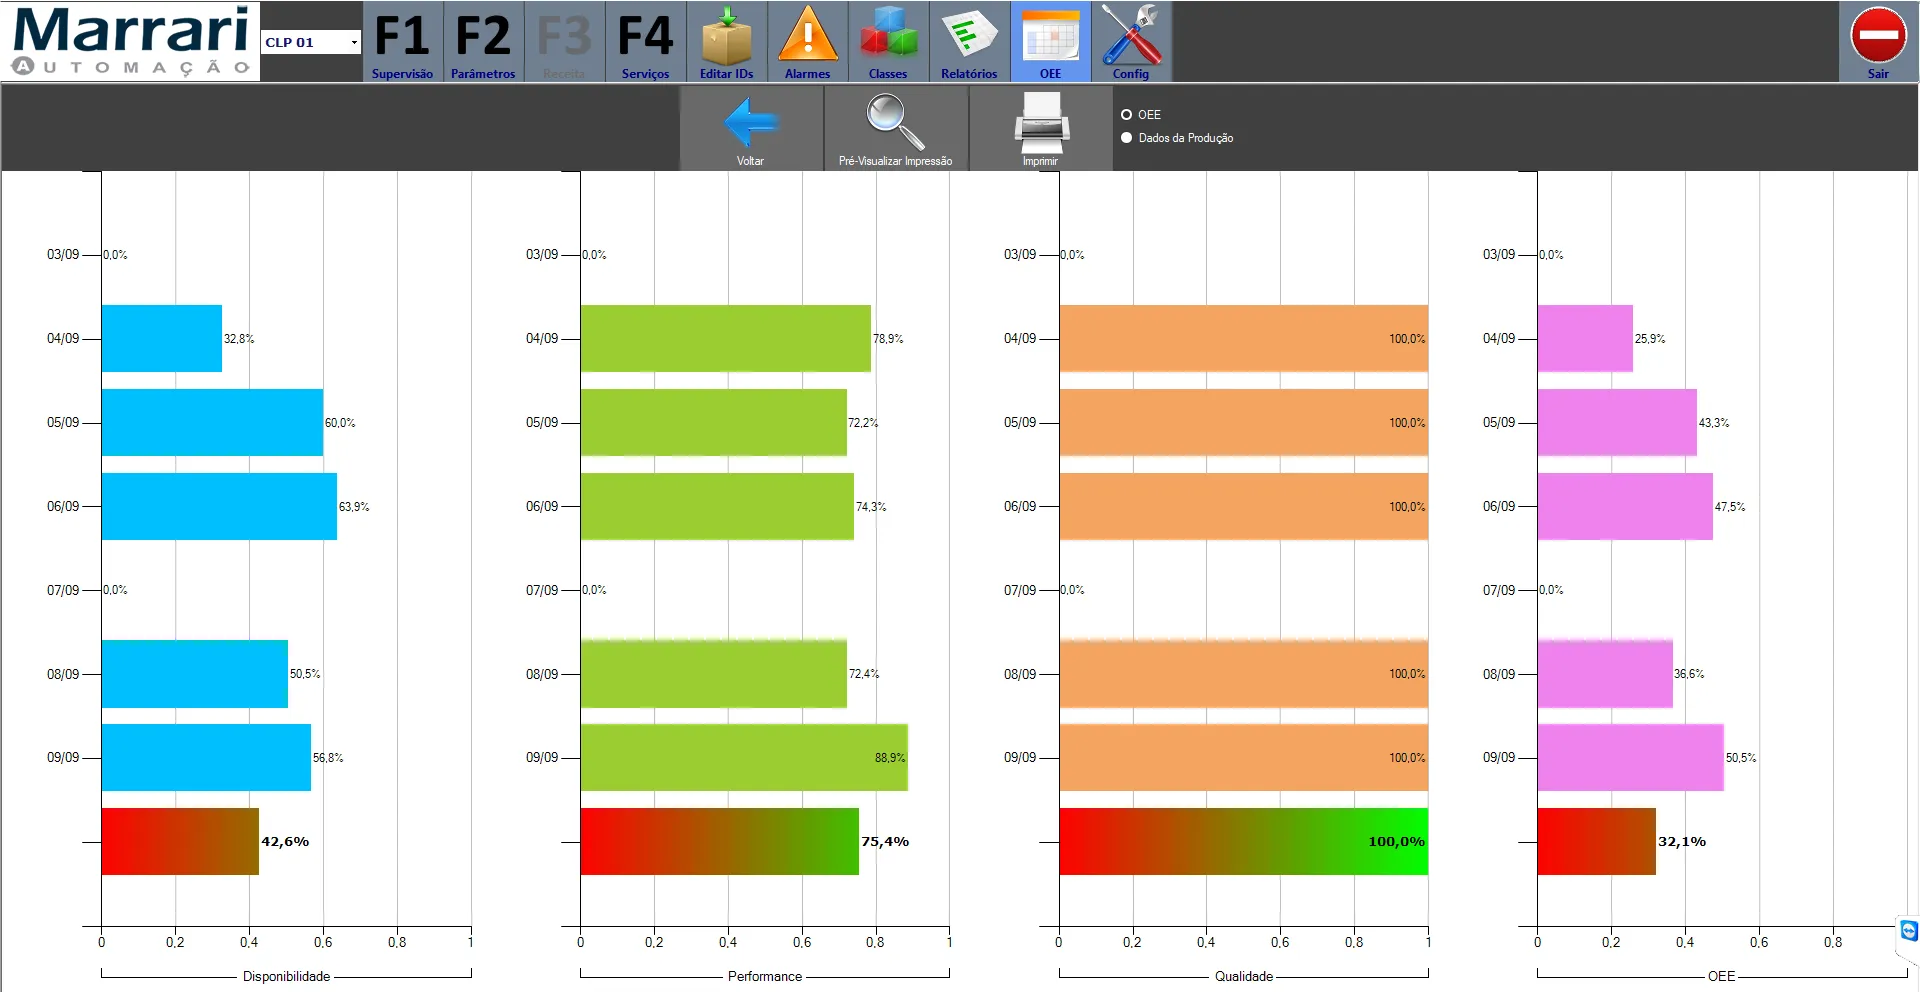
How to read this screen
- Each row is a day, and each column is a factor: availability, performance, quality and OEE.
- The last row shows the result for the period.
- So you see on which day and in which factor the line lost out.
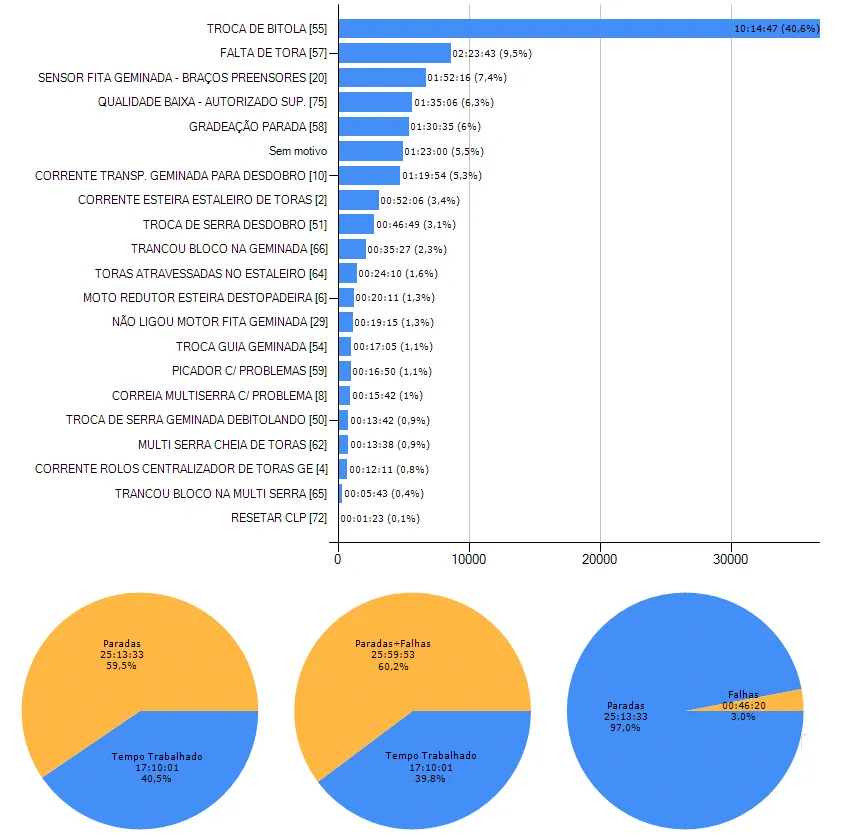
How to read this screen
- The bars add up the stopped time for each reason, from longest to shortest.
- The operator enters the reason for each stop, and the chart shows what to tackle first.
- The pie charts compare time worked with stops.
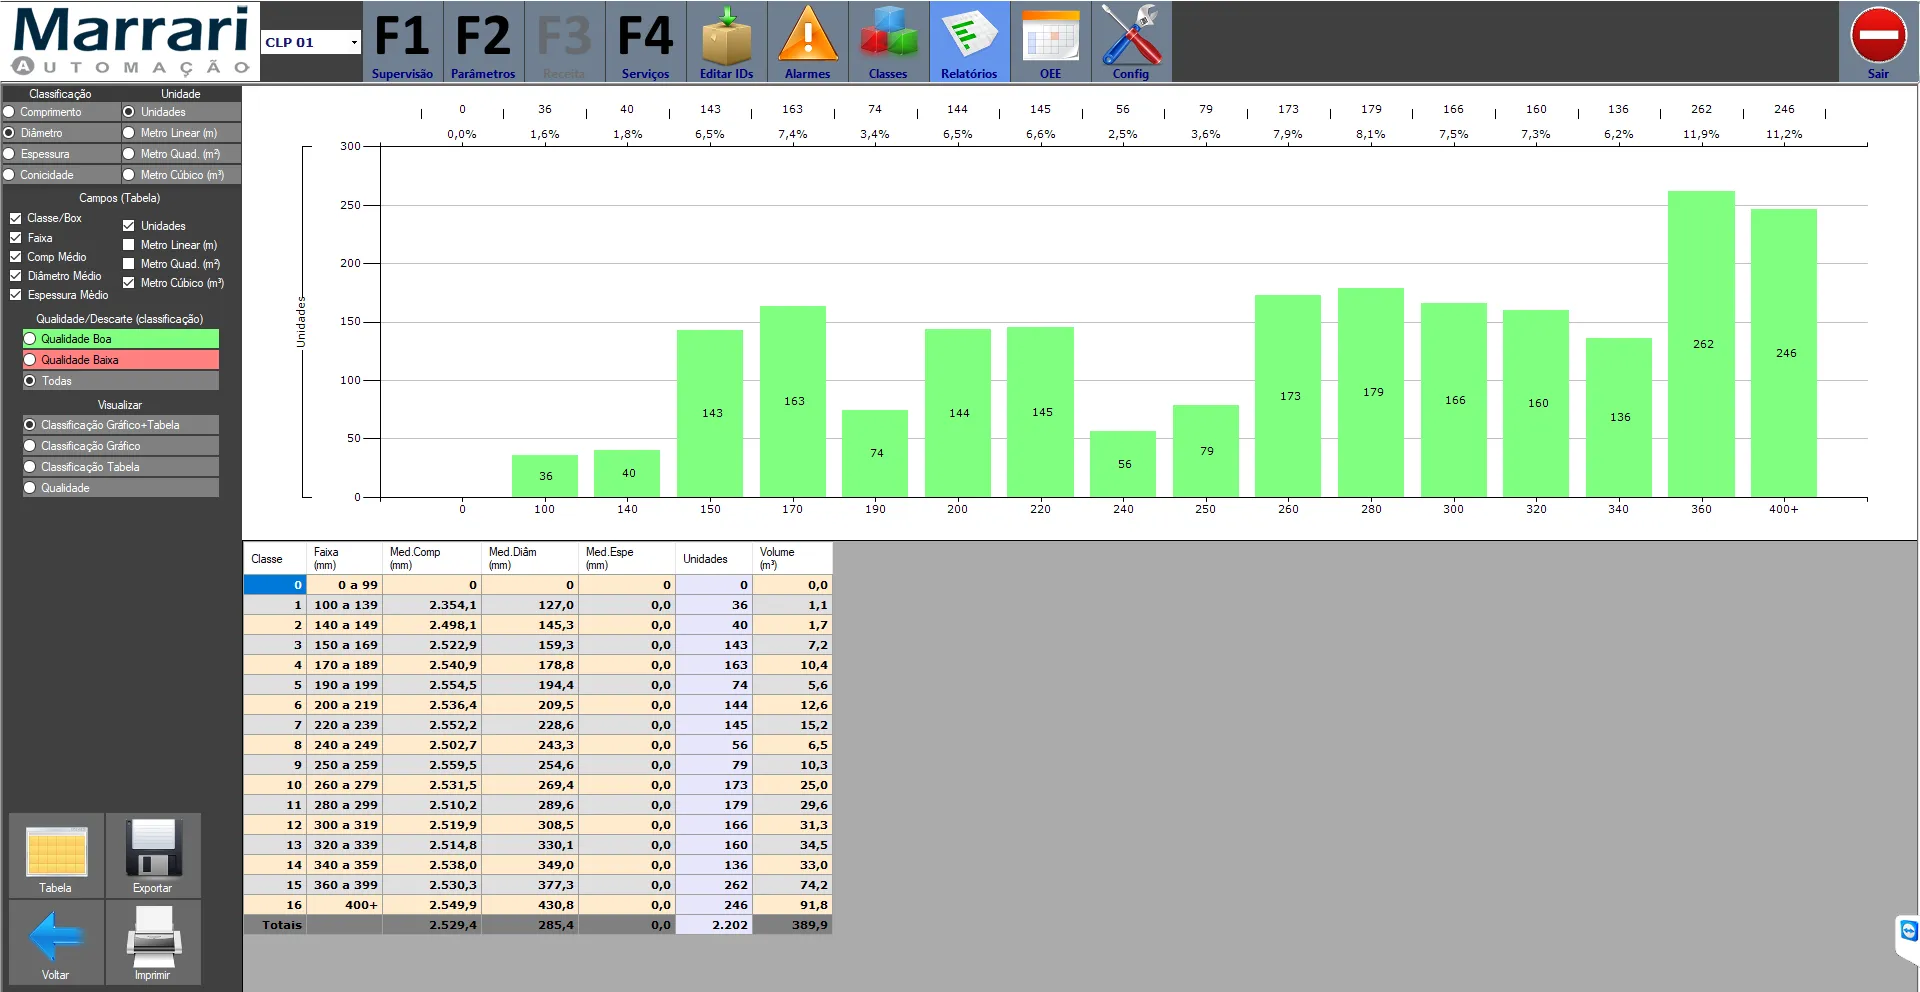
How to read this screen
- Each bar is a diameter range, with the number of logs.
- The table gives average length and diameter, units and volume for each class.
- With the batch identified, you can compare raw material from each supplier.
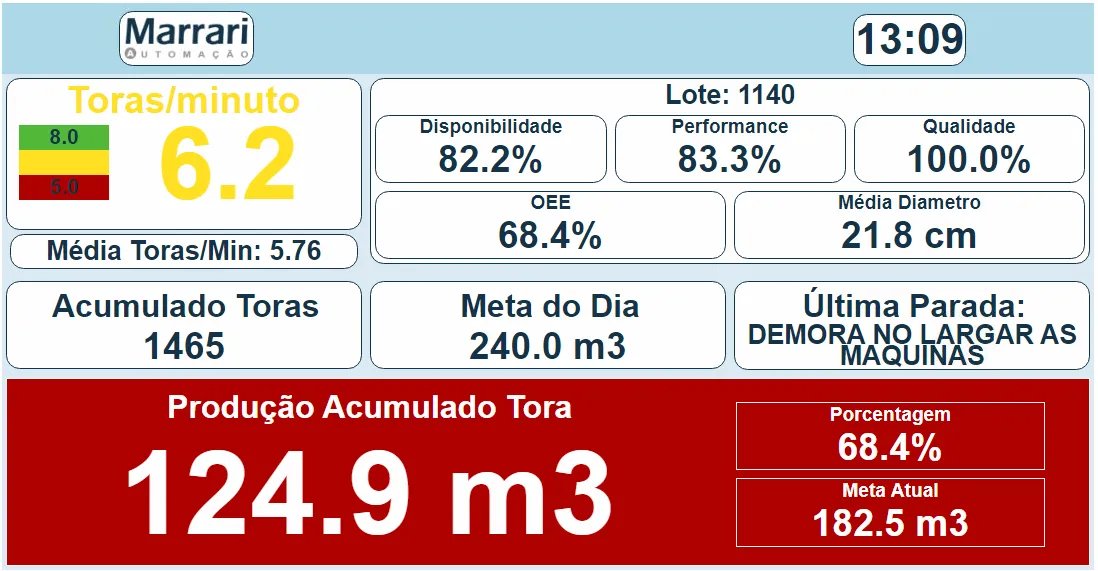
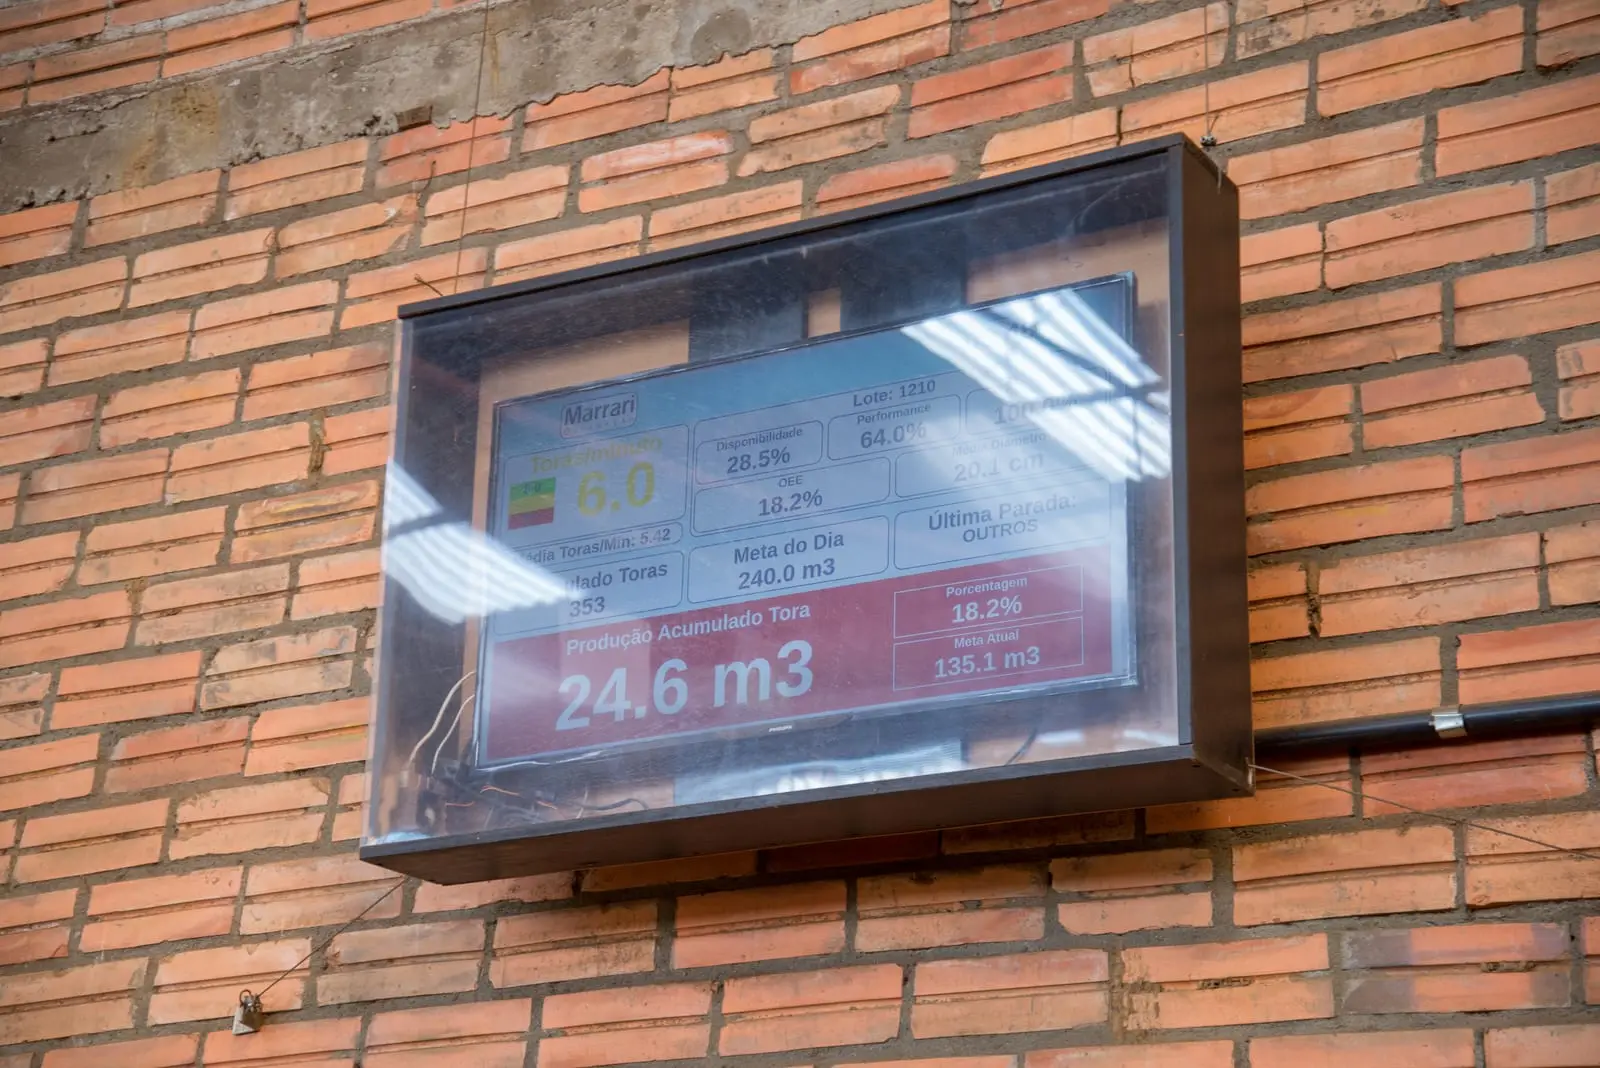
How to read this screen
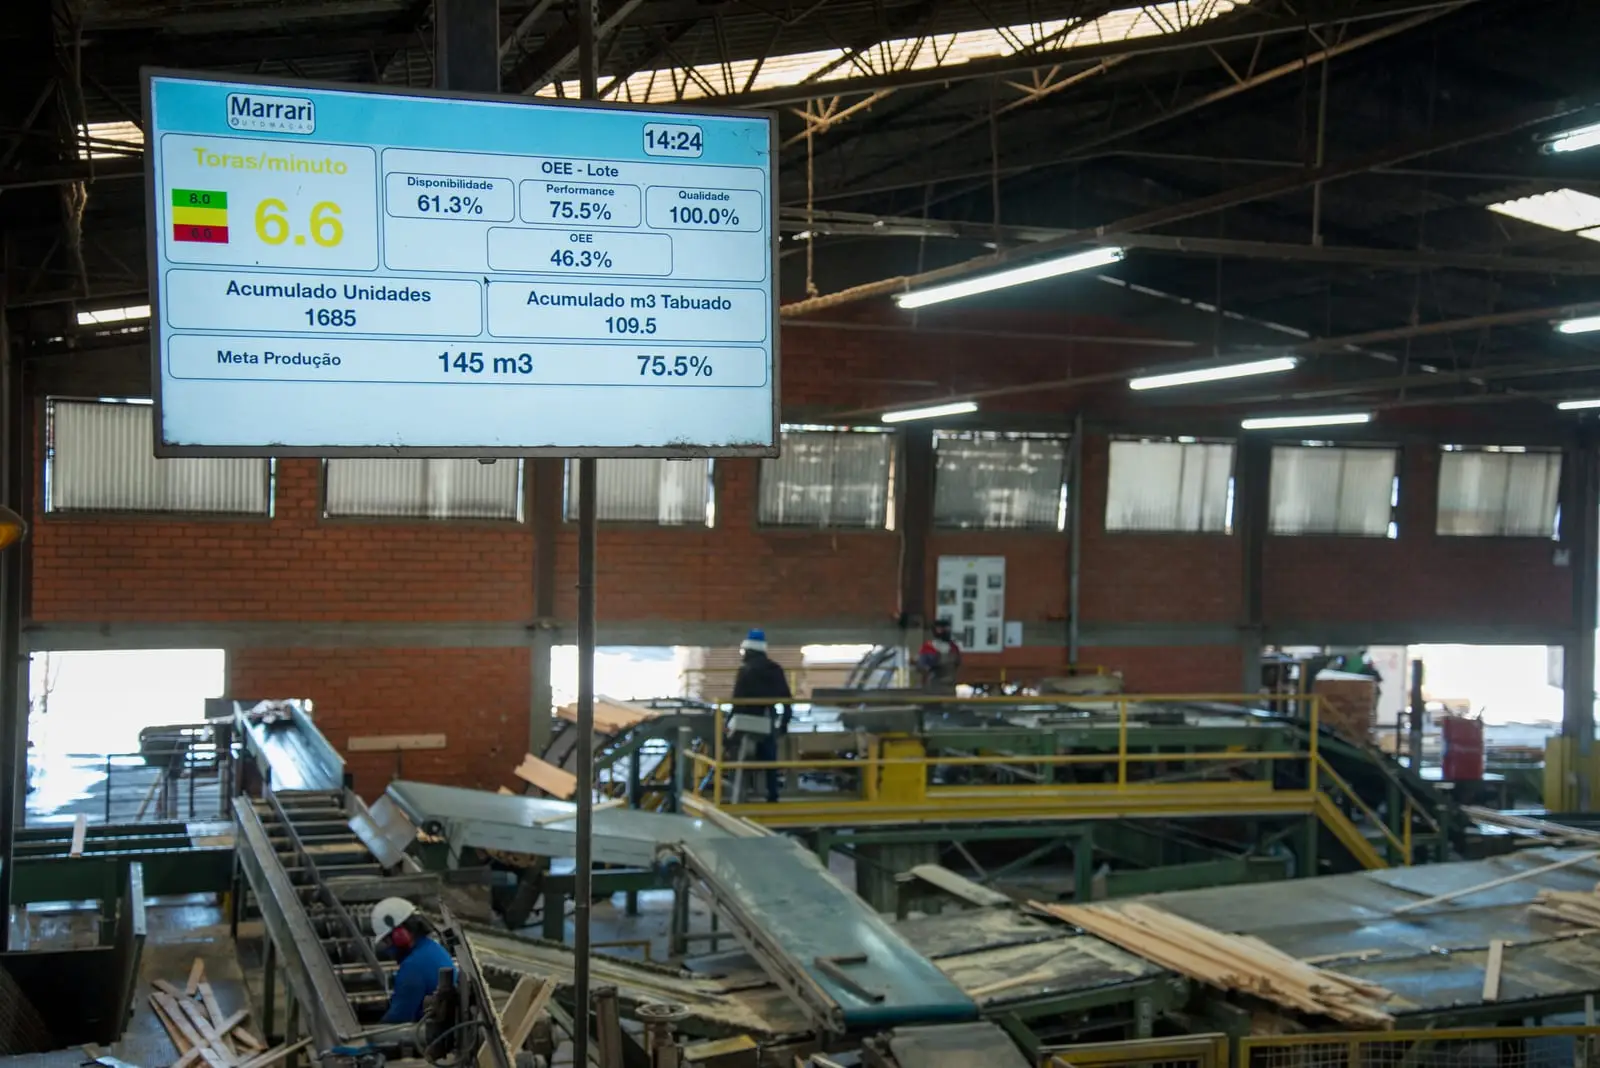
- This is the factory TV screen: the whole team sees the line’s pace.
- It shows logs per minute, the OEE factors, the daily target and the last stop.
- At the bottom, in large type, the accumulated volume and the percentage of the target.
How does the Pro X app work?
On the phone, the
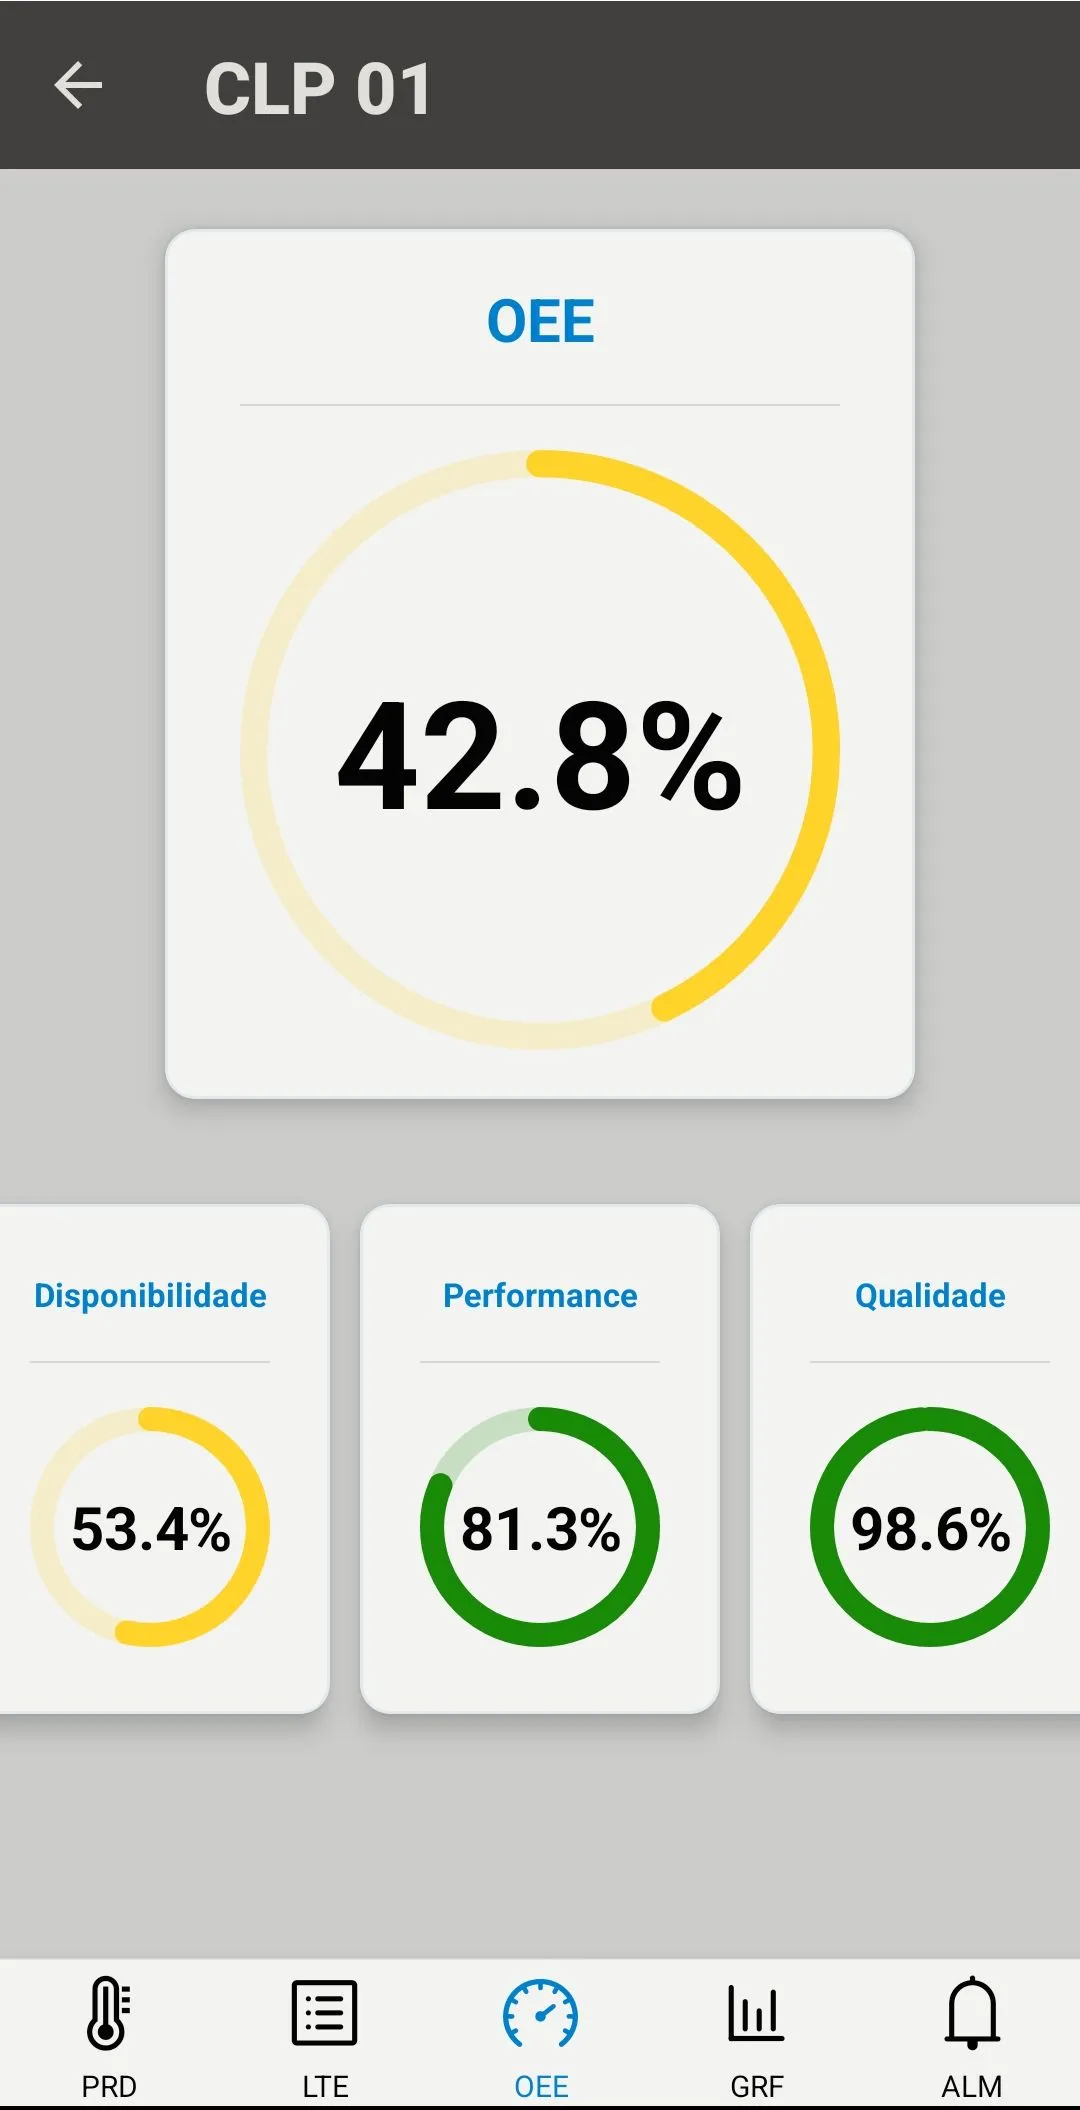
How to read this screen
- The machine’s OEE appears as a single percentage, in the large ring.
- Below, the three factors that make up OEE: availability, performance and quality.
- Each PLC on the line has its own screen; here, CLP 01.
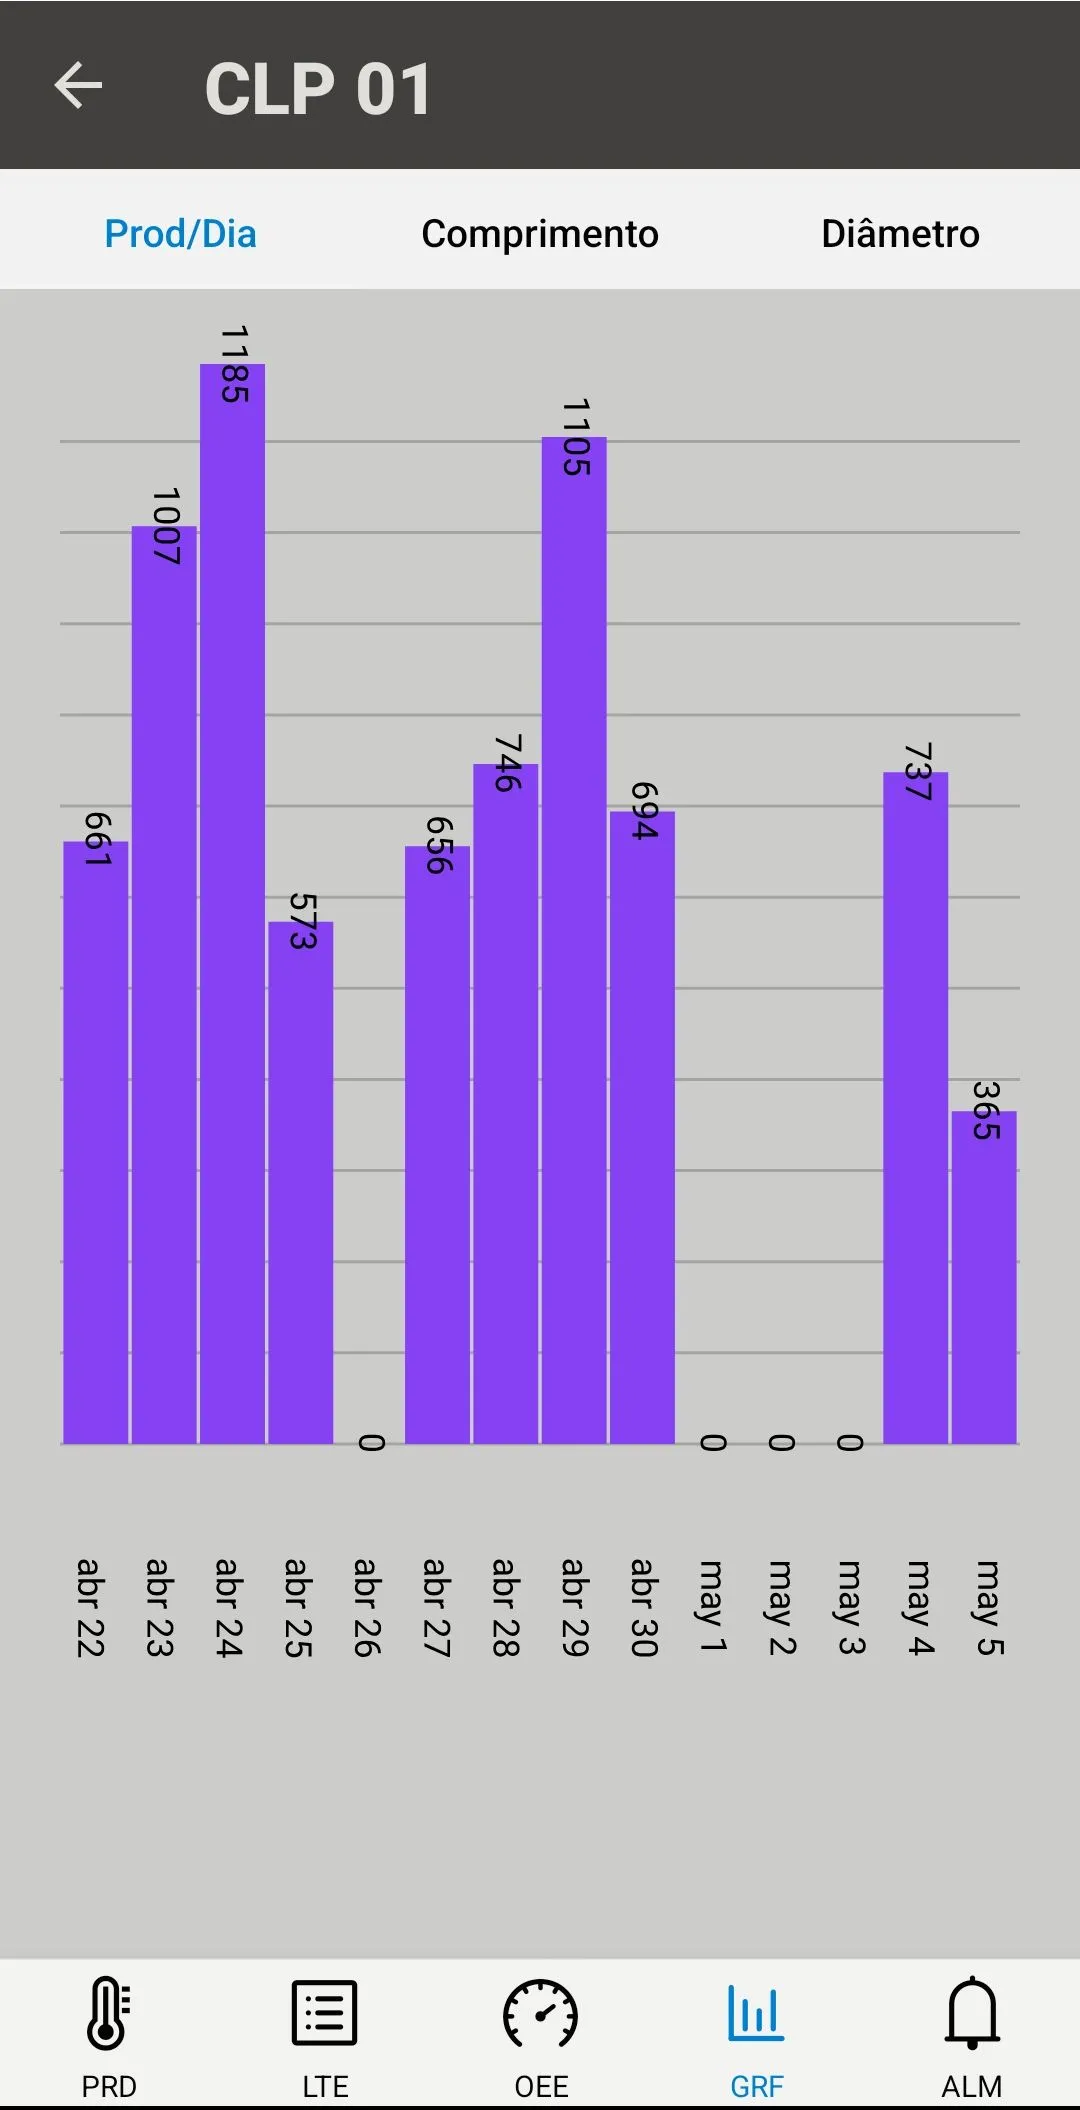
How to read this screen
- Each bar is one day’s production, with the number on top.
- A day with no production shows as zero, so long stops stand out.
- The other tabs show the same production by piece length and diameter.
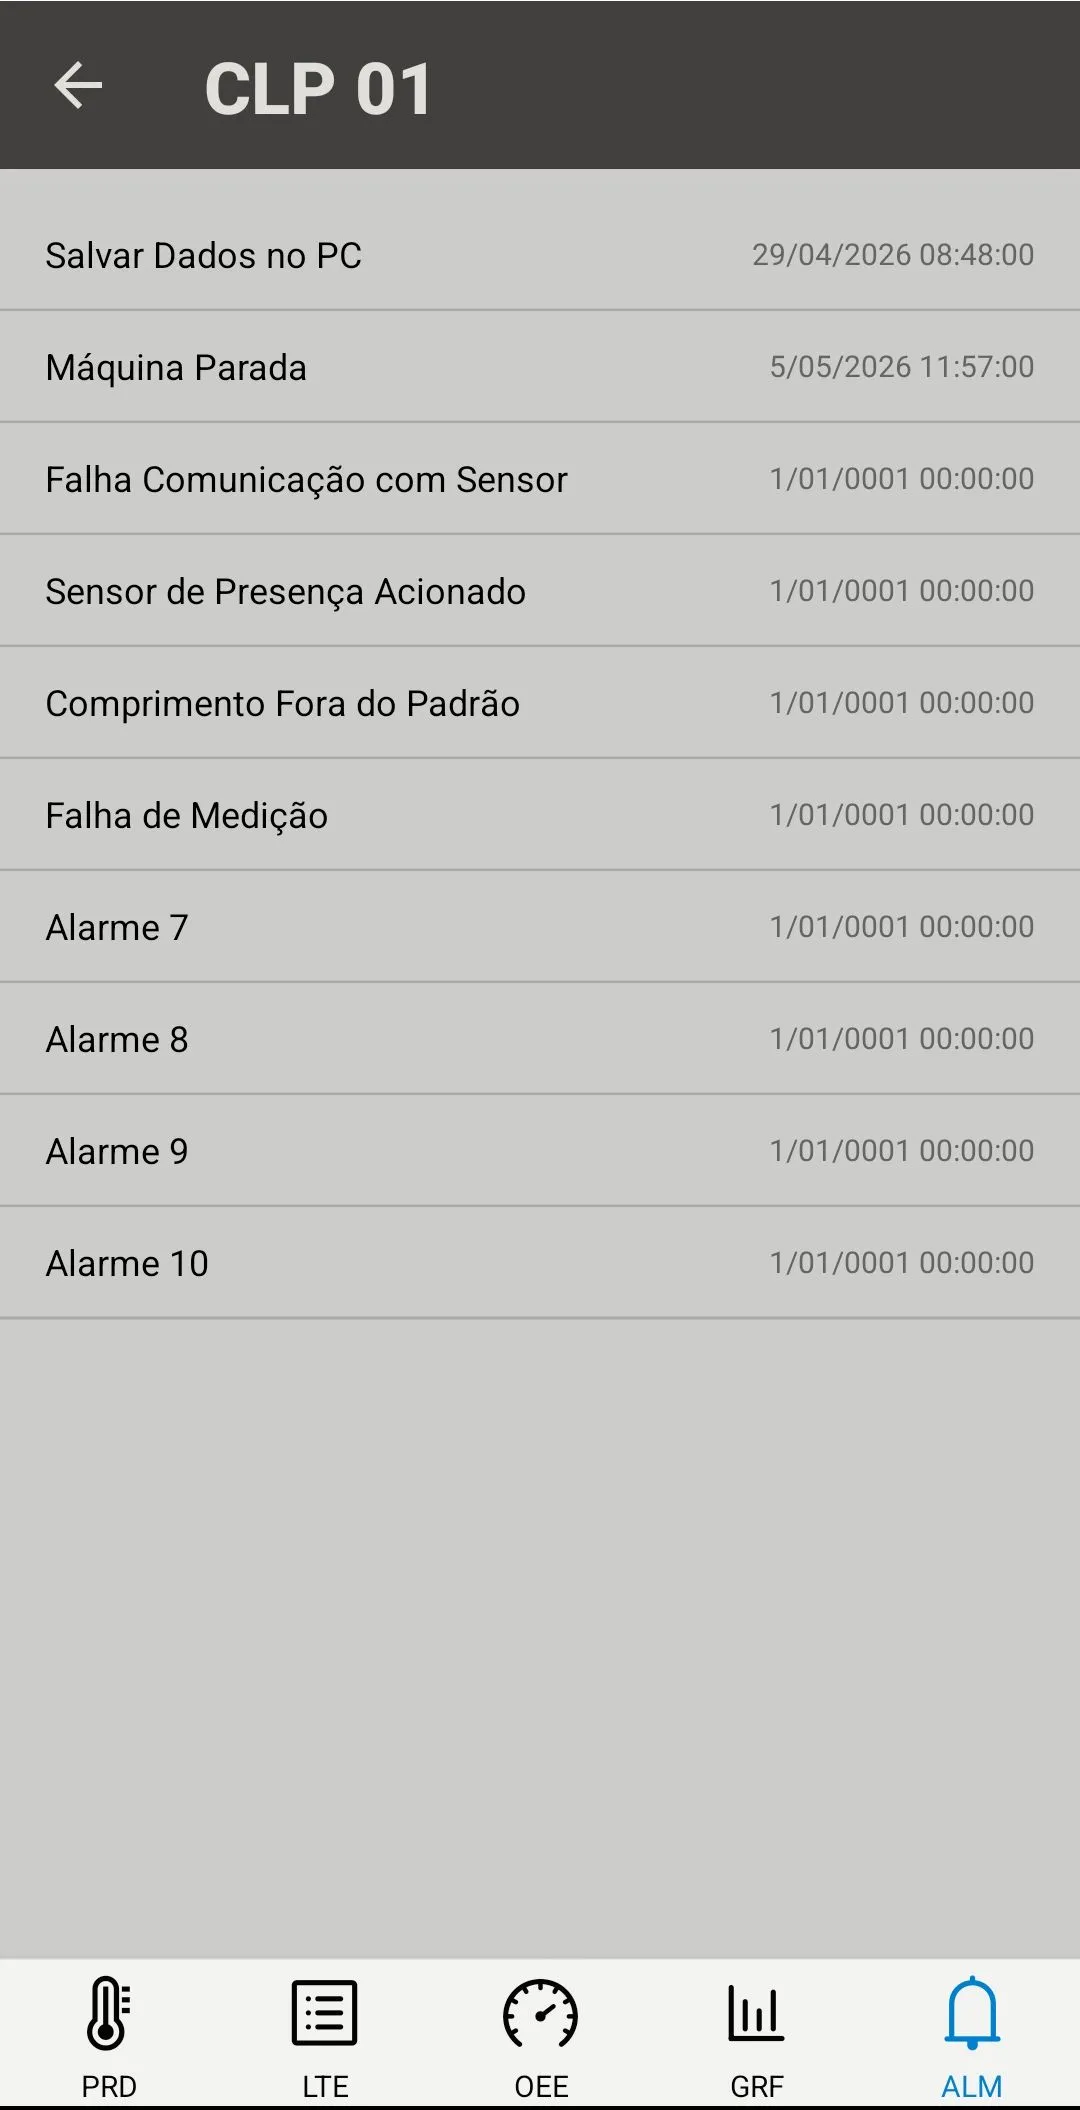
How to read this screen
- The line’s alarms in a list, each with the date and time of the last record.
- Machine stopped, sensor communication failure, length out of standard and measurement failure.
- The manager sees on the phone when and why the line stopped, without walking to the machine.
Who uses Pro X
At Grupo MGPaletes, in Brazil,
- 40% → 65%sawmill availability (Grupo MGPaletes)
- Less downtimeand more output (Tesser Madeiras)
- Down to
30 s short stops count too (Grupo MGPaletes) - Predicted upkeepfrom the reports (Tesser Madeiras)
Companies using


Pro X photos
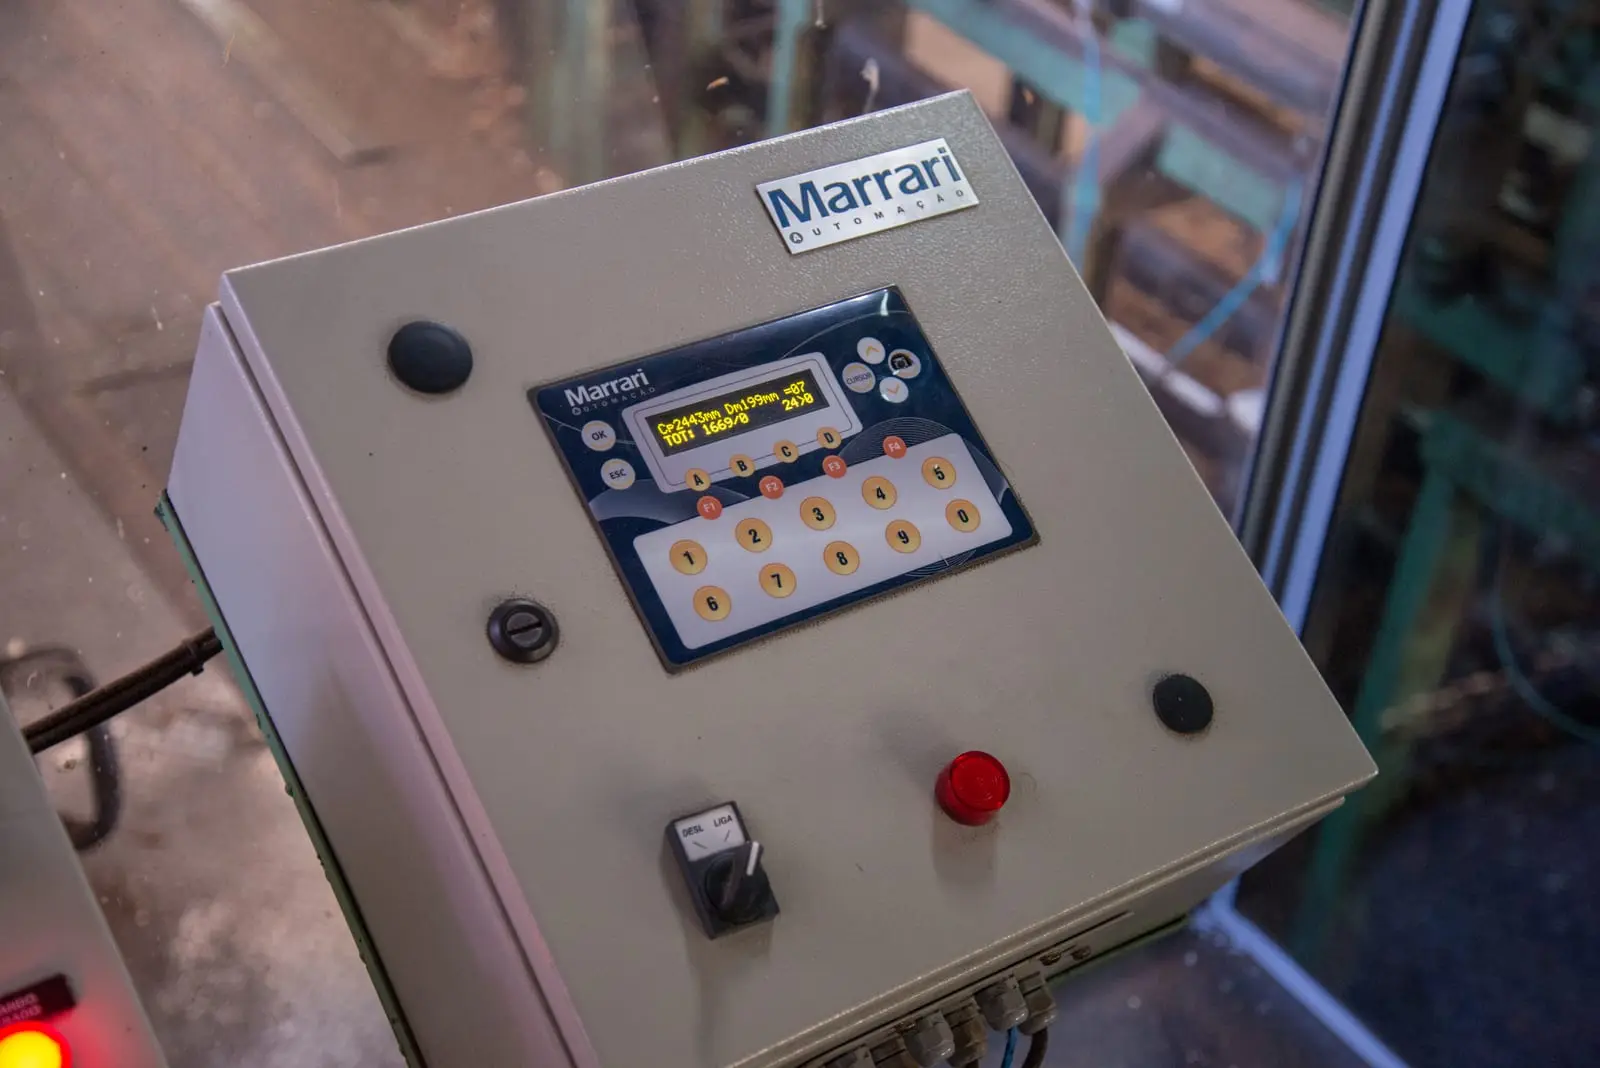
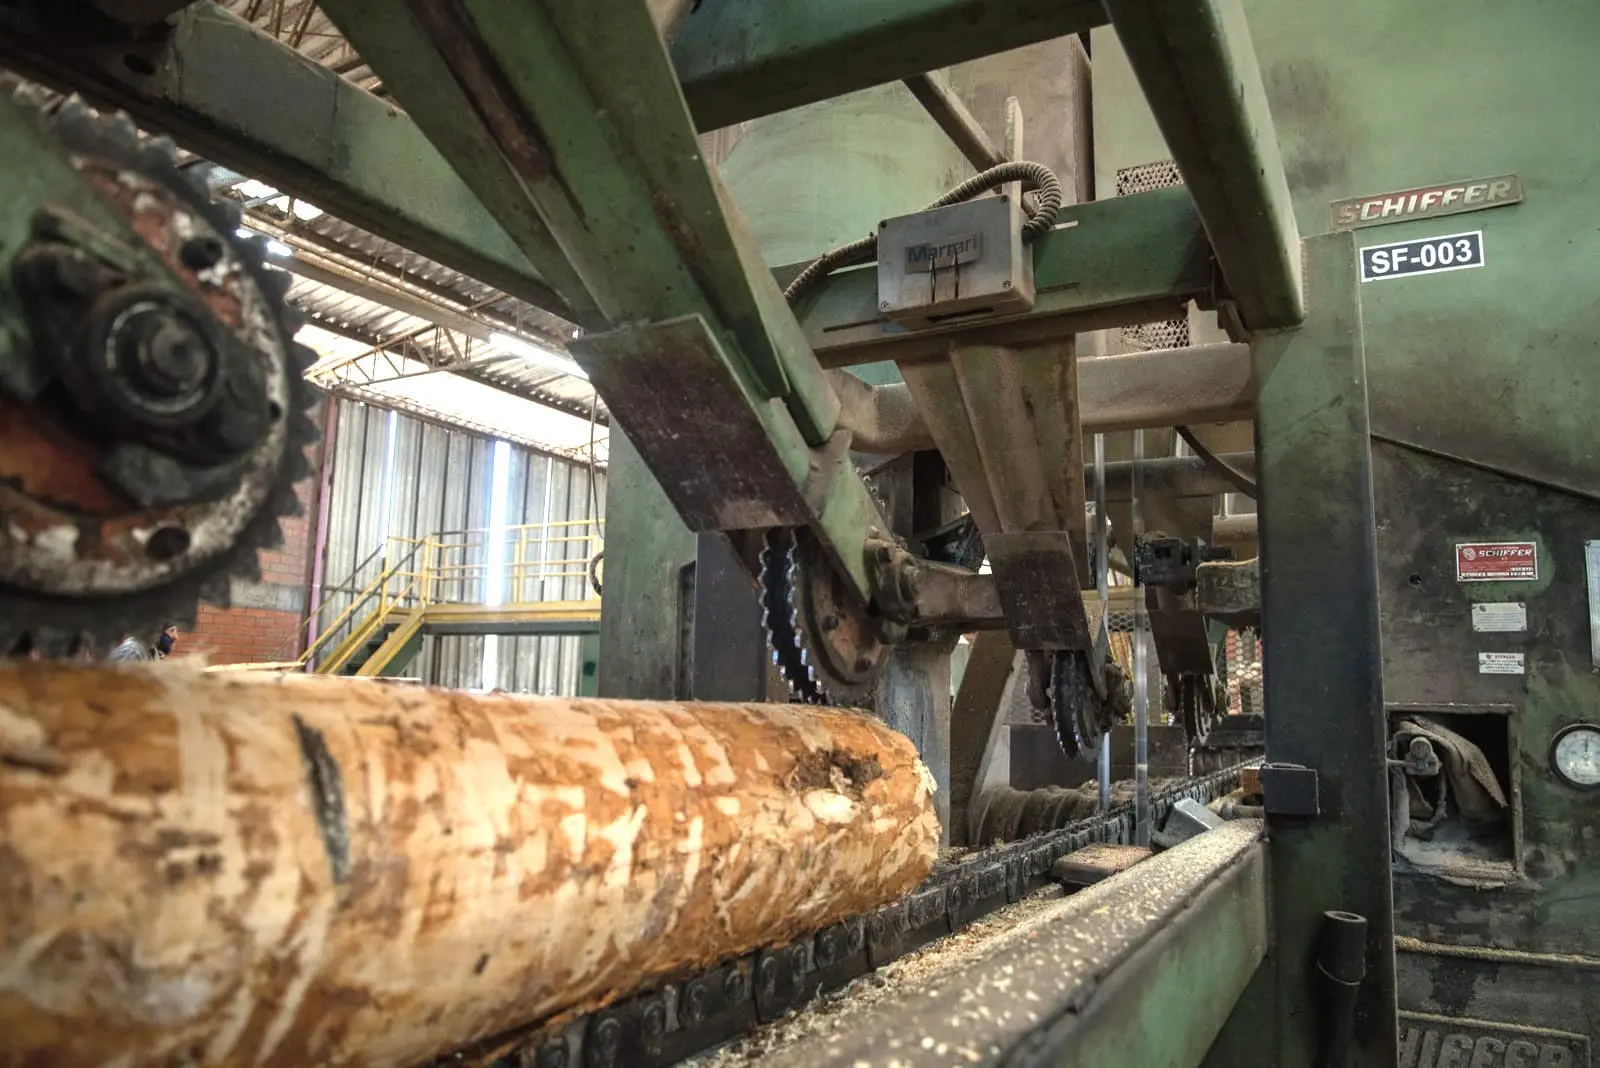
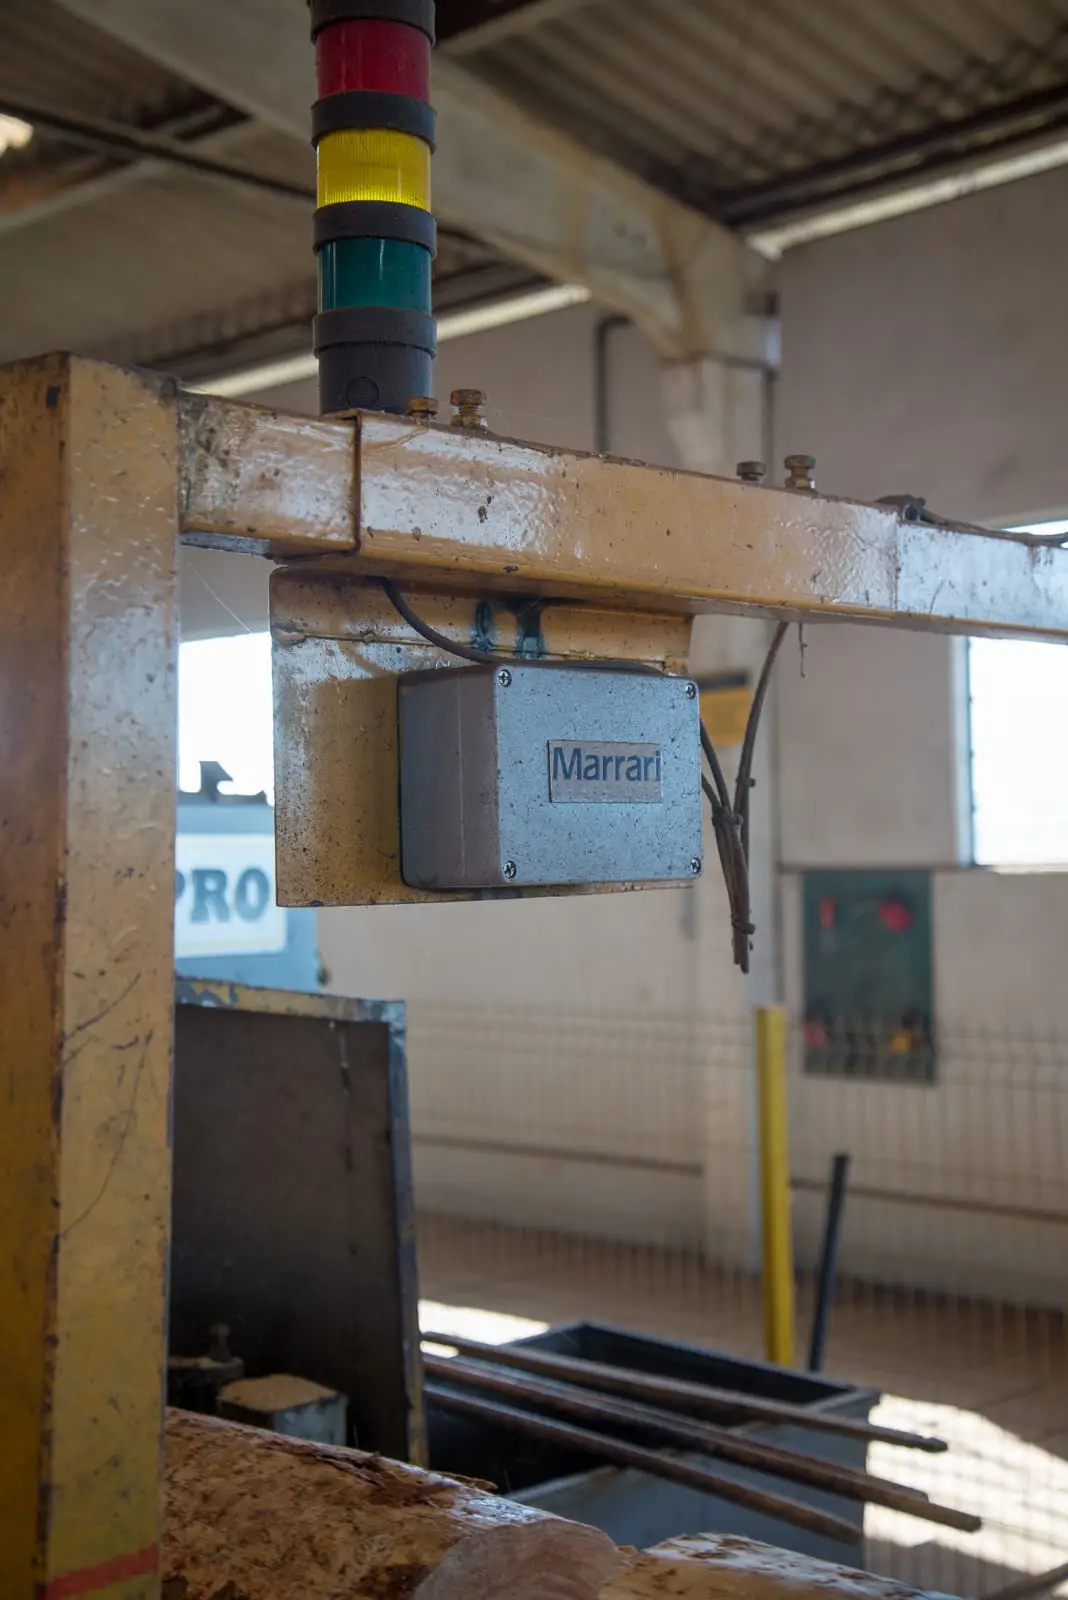
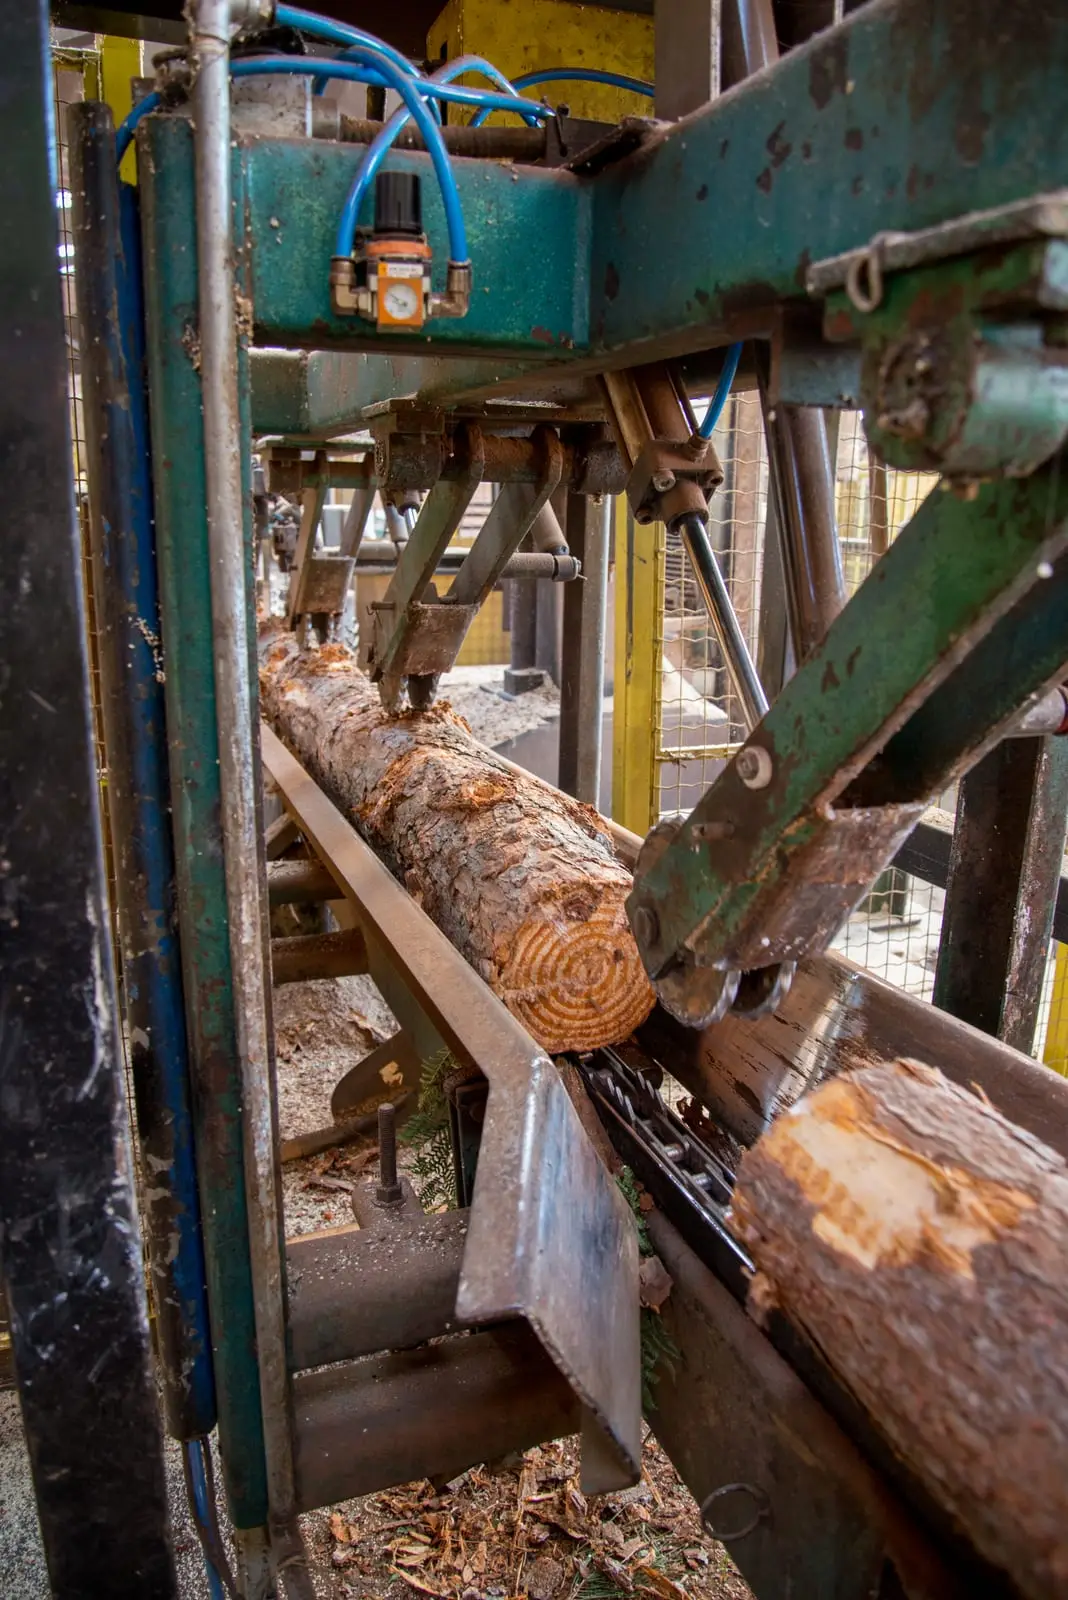
Real photos of the equipment and installations. Click or tap a photo to enlarge it.
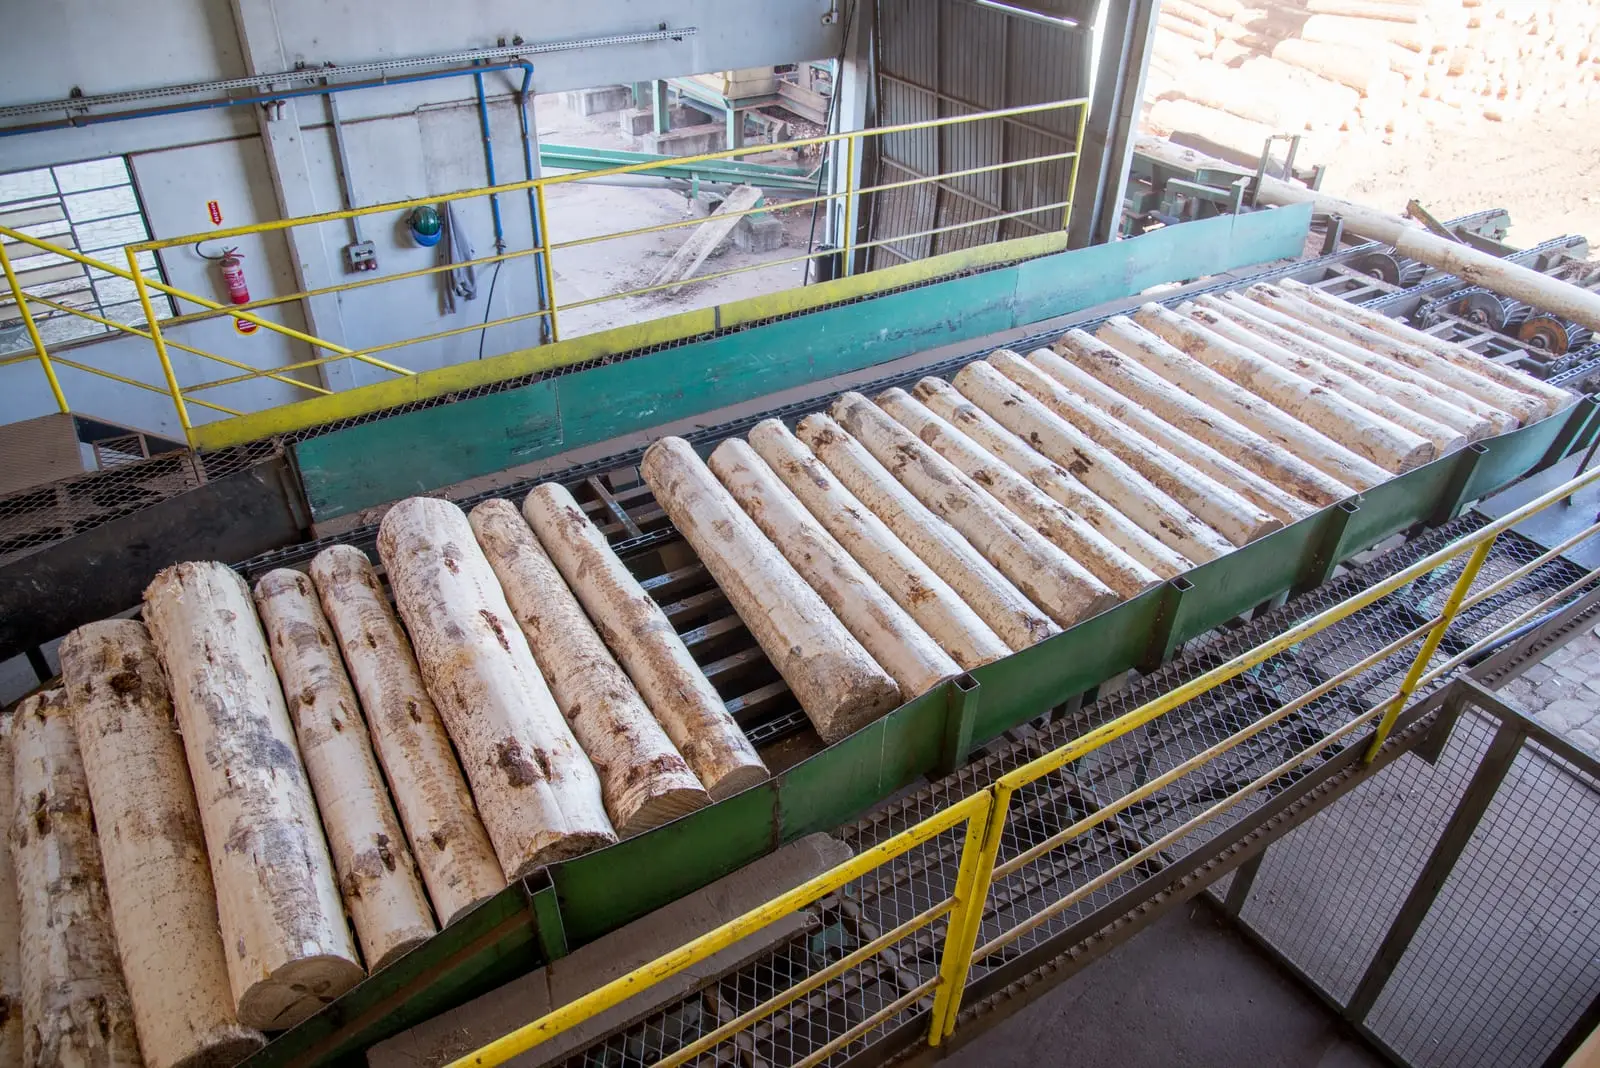
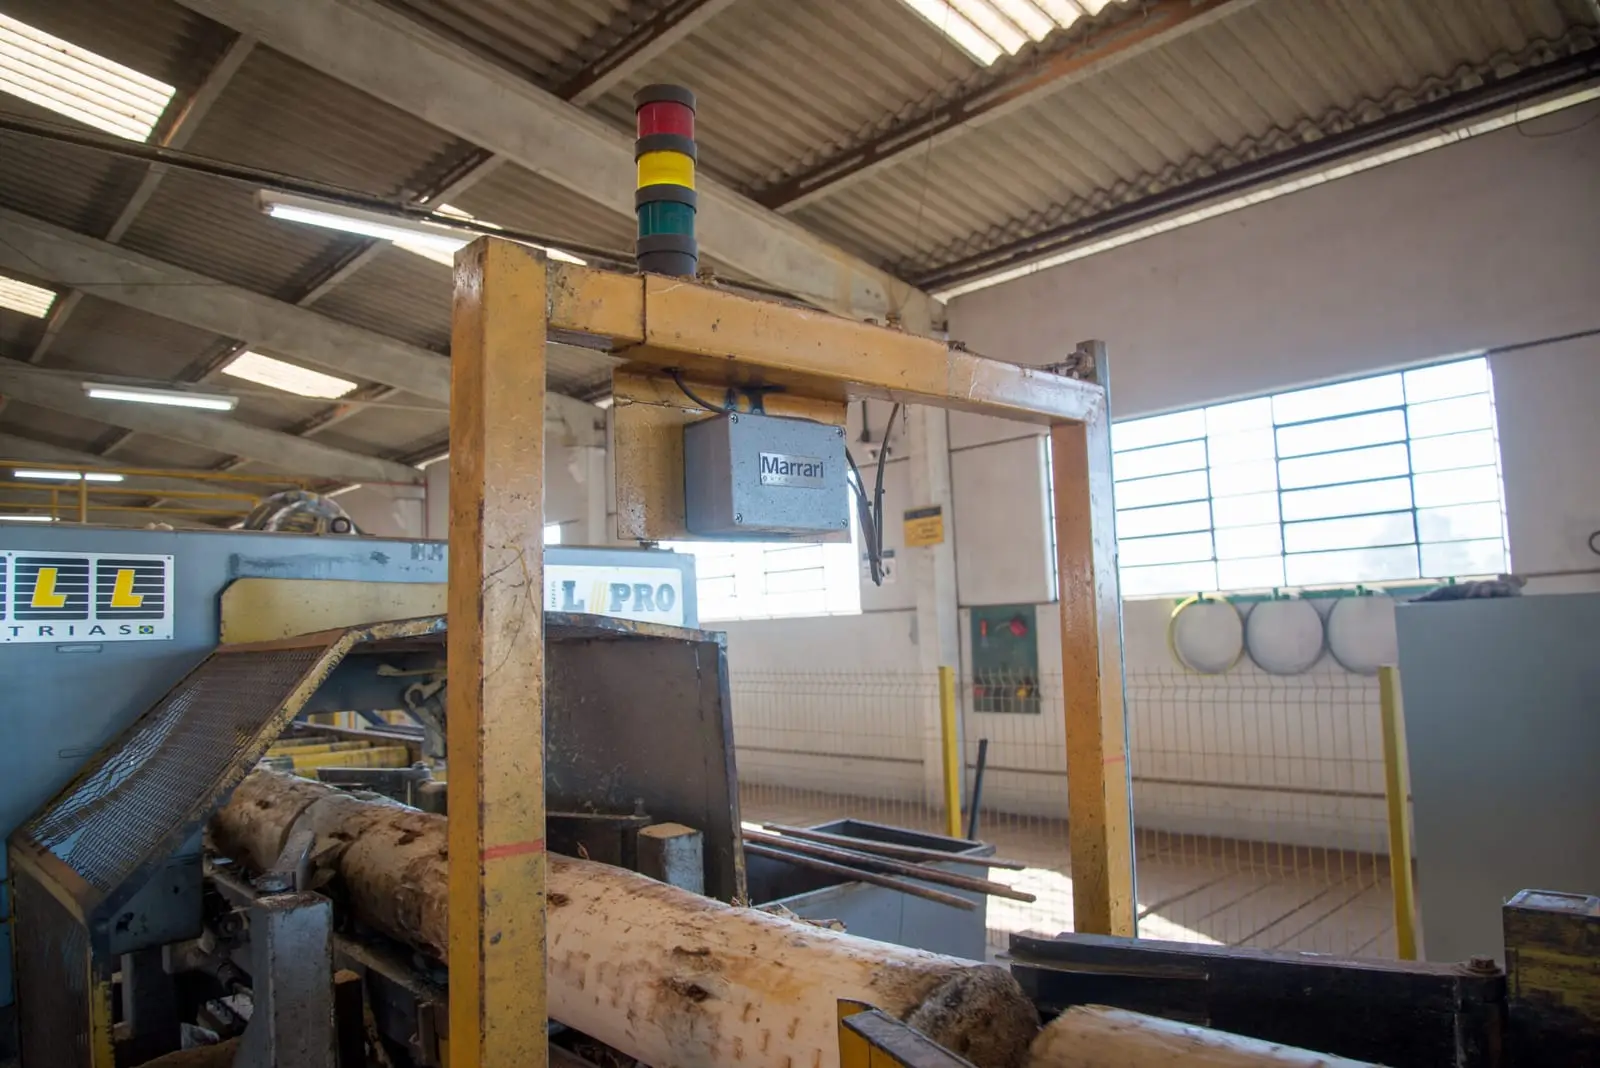
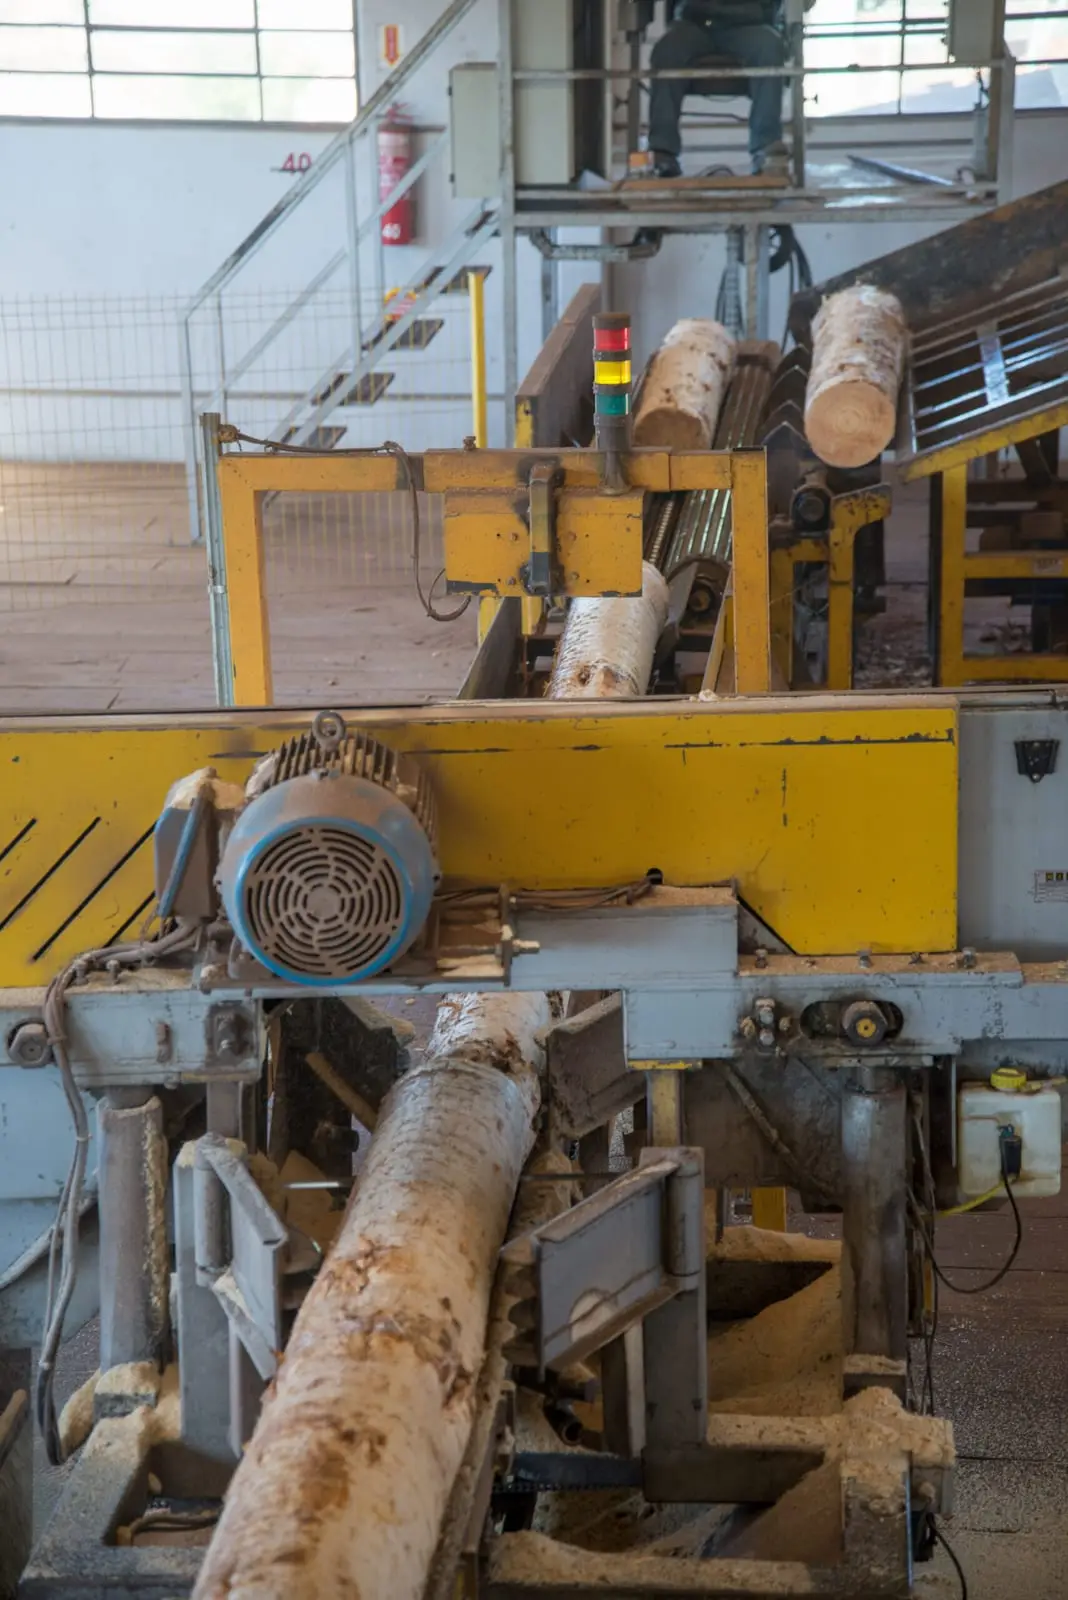
Pro X specifications
Measurement
| Measuring principle | optical laser sensors and |
|---|---|
| Models | Basic (piece count or linear meters), Standard (logs and boards on a continuous line) and Carro (log carriage) |
| Sensor range | 50 |
| Accuracy | 1% of the measured distance |
| Measurements | length, width, thickness, speed (m/min), pieces/min and output in m, m² and m³ |
| Management | OEE, production history, stops with reasons and reports by batch, supplier and shift |
Installation and integration
| Communication | RS232 and RS485; ERP integration |
|---|---|
| Screens | mobile app (sold separately) and dashboard for factory TVs |
| Access | |
| Power supply | 95 |
| Operating temperature | up to |
| Warranty | 6 months |
Frequently asked questions about the production controller
Can the system control other types of production?
What is OEE in Pro X?
Does Pro X have an app?
What is the Pro X warranty?
How does buying from outside Brazil work?
No question with that term. Try another word or talk to the team on WhatsApp.
Request a quote: Pro X
Free and with no obligation. A Marrari specialist replies within 24 business hours.
- Installation and integrationBy Marrari engineering, which chooses the best point on the line.
Start-up is backed byafter-sales support and, for lean manufacturing, consulting from partner Elevare. Outside Brazil, Marrari’s export team coordinates the service. 6-month warrantyFor all Marrari systems and equipment.- Support and calibrationSupport in Brazil and Latin America; new recipes from the UmiLab laboratory.